Manufacturing & Delivery Case · Barcelona, Spain

A complex restaurant package, made buildable.

Seven product families translated from renderings, CAD drawings and dimension schedules into 67 trial-fitted assemblies, completed and shipped in 35 days.

67Assemblies
7Product types
35Calendar days
01 / The brief

A contractor needed one coordinated production path for stainless steel, acrylic, fluted glass, PVD finishes and warm lighting.

LocationBarcelona, Spain
Completed for shipmentSeptember 2026
Client typeContractor
Design inputRenderings, CAD, dimensions
Primary material304 stainless steel
InstallationClient team + remote guidance
02 / Scope

One coordinated package

Seven product types.
Sixty-seven assemblies.

Different geometries, finishes and mixed-material interfaces were controlled under one engineering, trial-fit and delivery workflow.

12

Geometric partitions

304 stainless steel, acrylic, vacuum-plated finish and warm LED lighting.

16

Openwork booth partitions

Gold PVD stainless steel with integrated warm lighting.

8

Birdcage booths

Large rose-gold brushed stainless-steel seating enclosures.

8

Circular partitions

Champagne brushed stainless steel, fluted glass and warm lighting.

6

Fluted-glass screens

Rose-gold brushed stainless steel with warm LED integration.

1

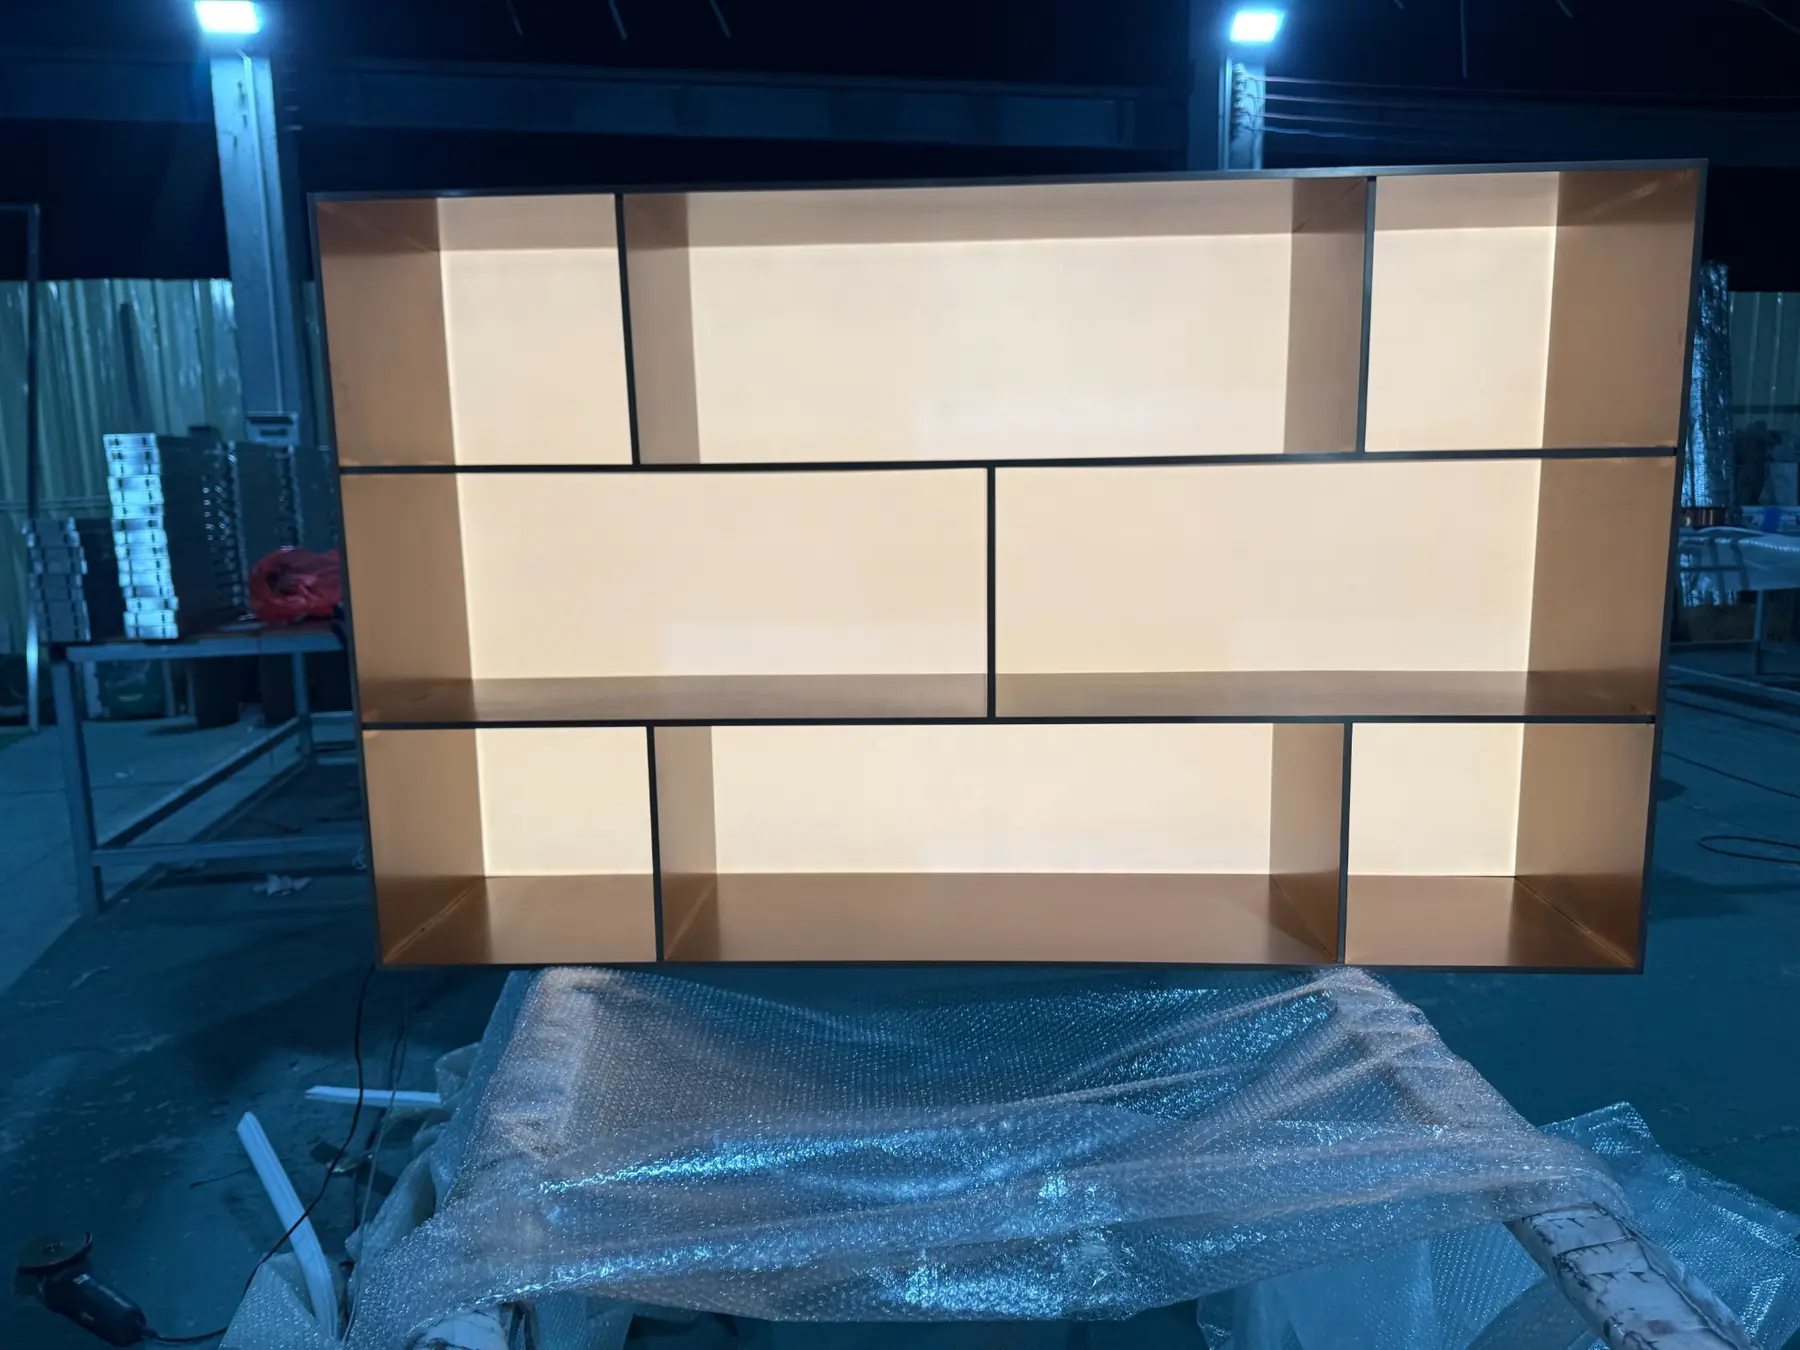
Illuminated bar cabinet

304 stainless-steel frame, acrylic backing and concealed warm lighting.

16

Suspended ornaments

304 stainless-steel decorative elements with warm lighting.

The critical item

Engineering a 3.2-metre birdcage booth.

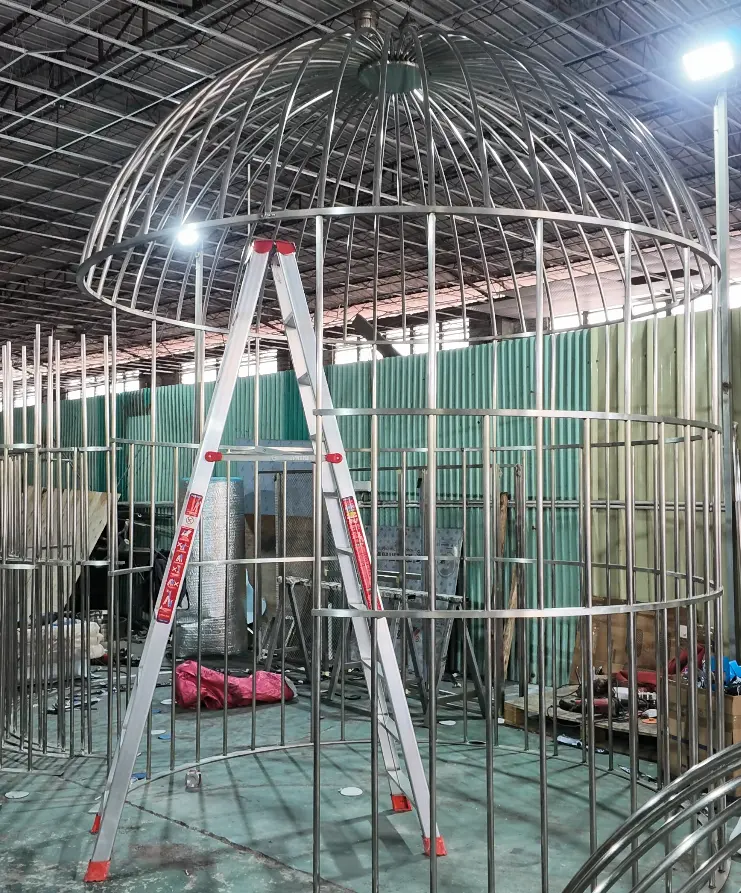
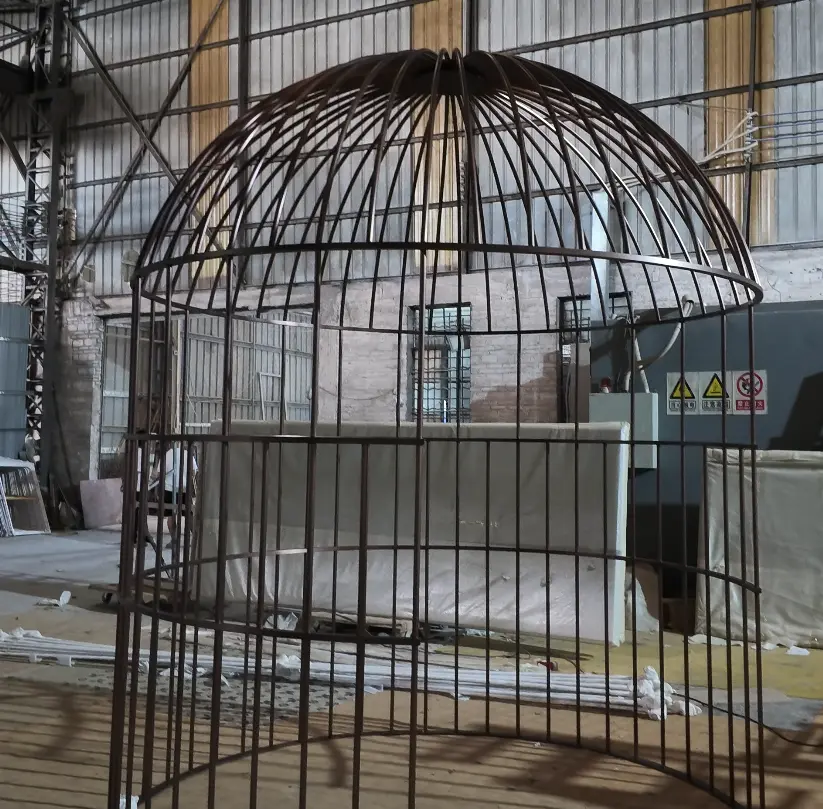
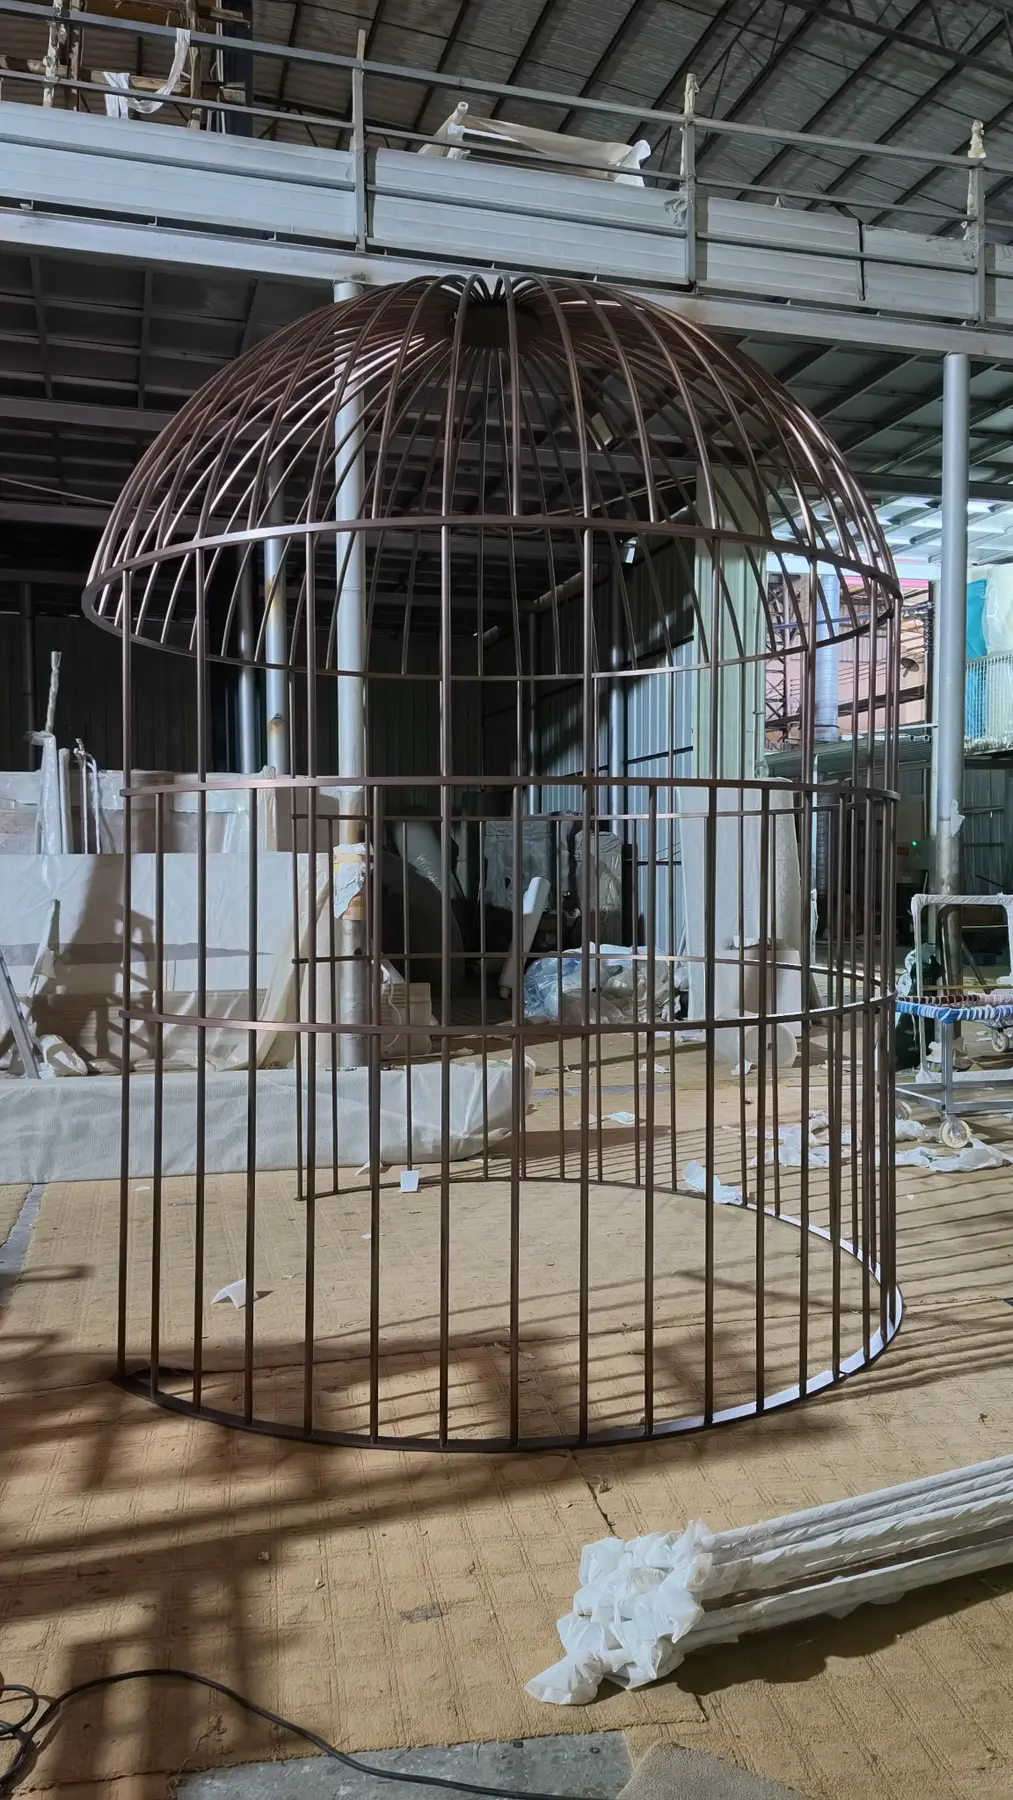
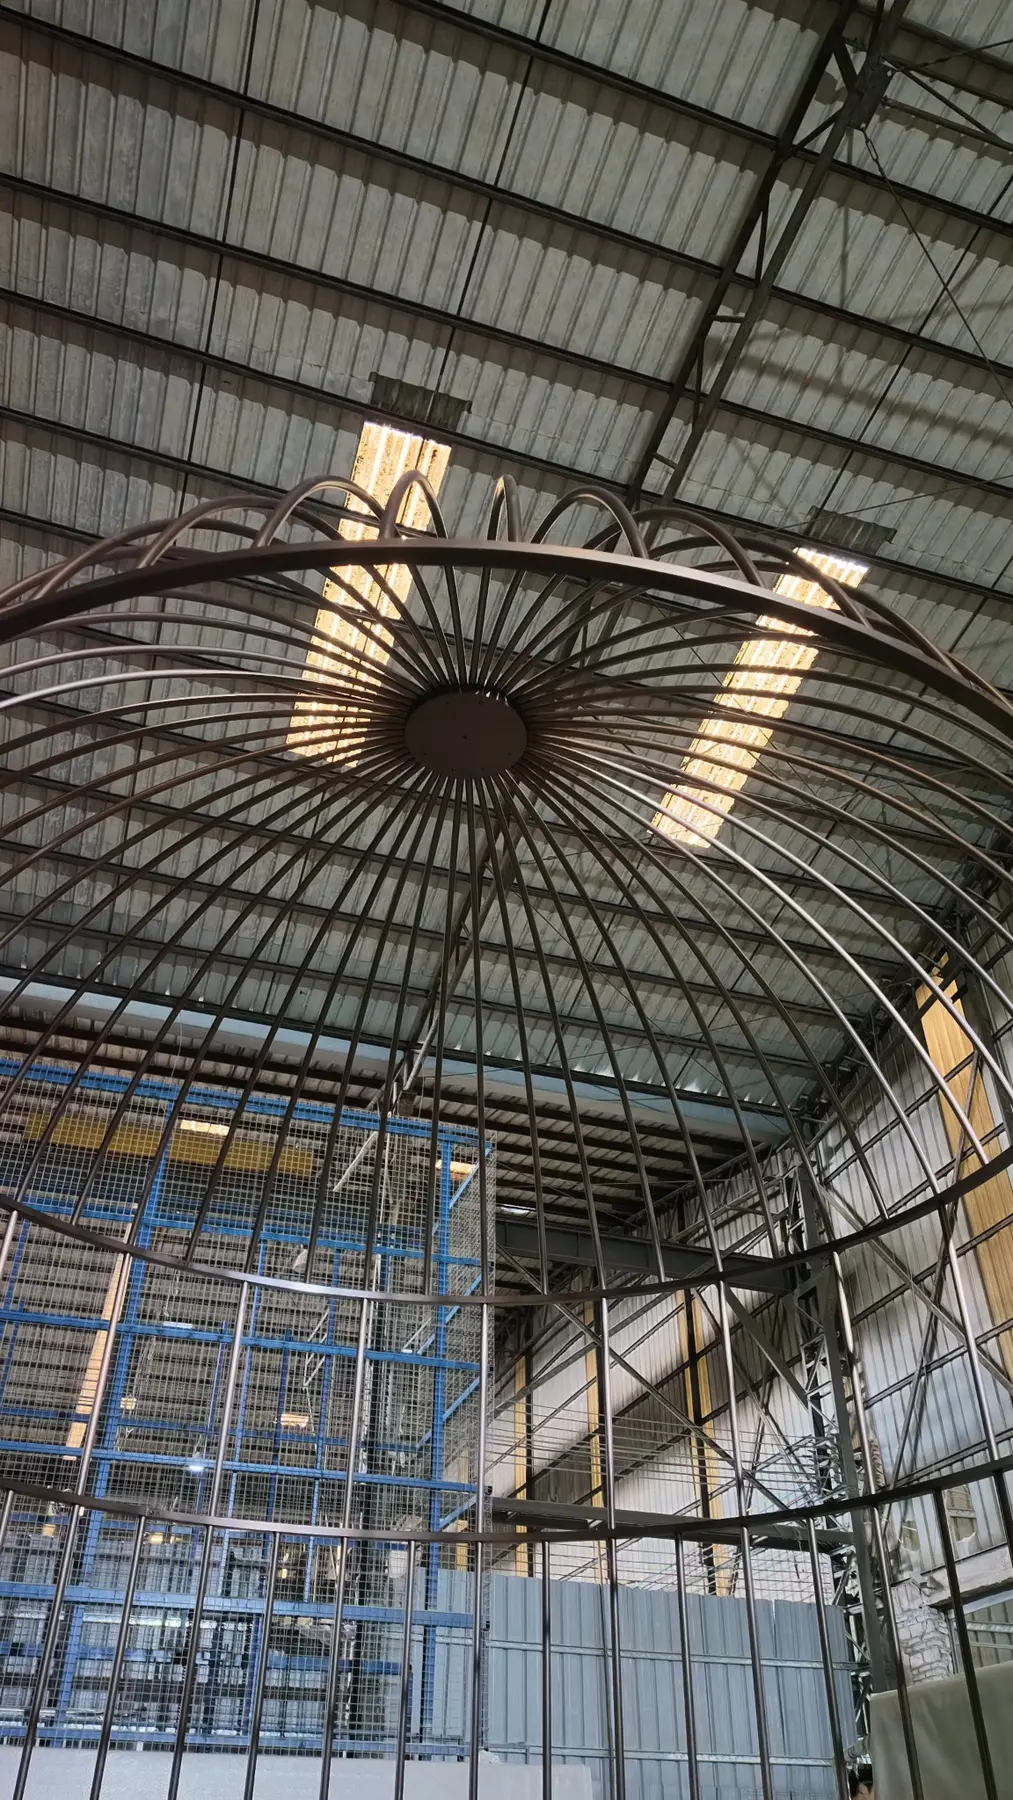
Each of the eight booths had a converging domed roof. Dozens of bars of different lengths and curvatures had to meet at a compact top ring while preserving comfortable seating clearance and an open visual rhythm.
3.2 mOverall height
2.3 mDiameter
8Identical units
Curvature controlBars were grouped and numbered by curvature for repeatable production.
Hidden modular jointsEach cage was divided into four main panels, with split lines placed at decorative bands.
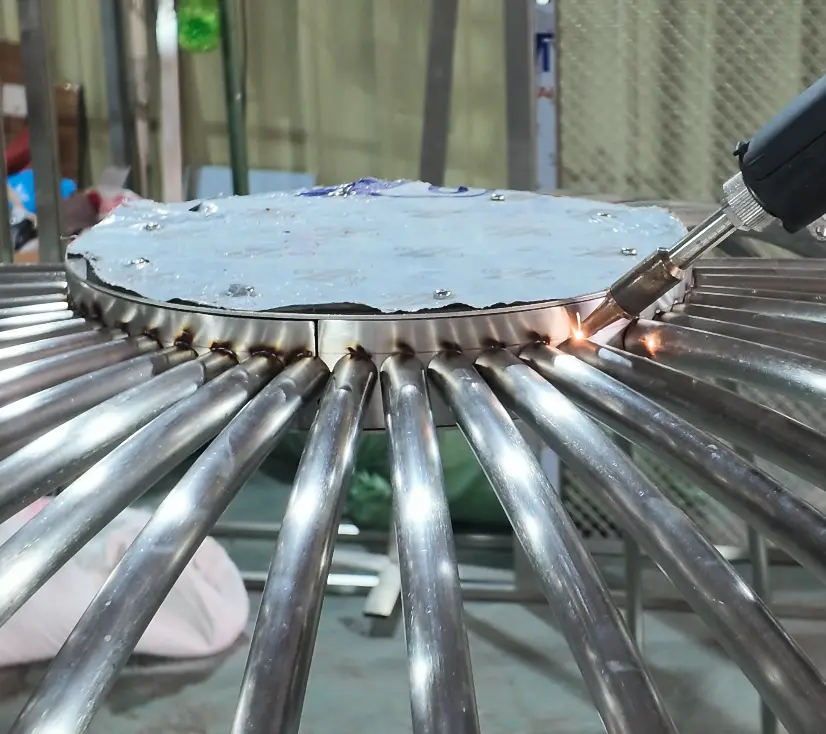
Quartered top ringThe final top ring was divided into four sections and screw-locked during assembly.
Seating clearanceInternal depth and head clearance were checked against seated use instead of copied directly from the rendering.
Final rose-gold brushed finishFinished rose-gold brushed stainless-steel birdcage booth trial assembled in the workshop
Domed top geometryInterior view of the converging birdcage bars and quartered top ring
Pre-finish trial assemblyBirdcage booth fully trial assembled before surface finishing
WeldingBirdcage stainless-steel bars being welded to the top ring
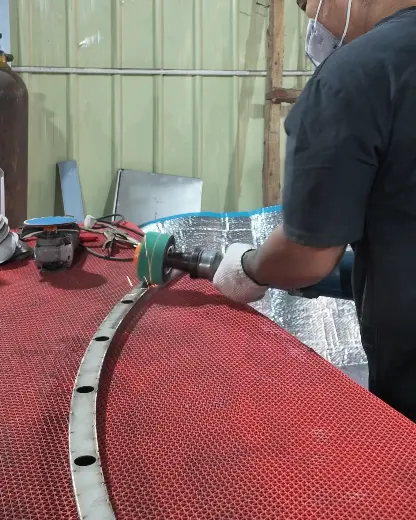
GrindingCurved stainless-steel ring being ground during fabrication
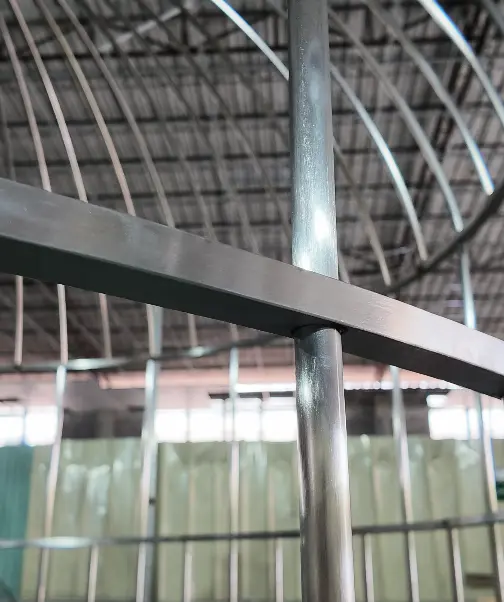
Joint detailingClose view of a birdcage rail connection during fabrication
Post-finish trial fitRose-gold brushed birdcage booth reassembled after finishing

Manufacturing response

The dome would not close reliably. The sequence changed.

During the first full assembly, individually correct curved bars accumulated alignment error at the top. Production was reorganised around the top ring as the fixed reference.

  1. 01Leave controlled trimming allowance on every curved bar
  2. 02Align and fit each bar progressively from the top ring
  3. 03Trim and resolve the lower connections only after the dome closes
  4. 04Complete full workshop assembly and stability checks
  5. 05Disassemble, identify and prepare each module for shipment
4Main panels
per birdcage

Designed to travel

Full-size in the restaurant.
Nested for shipment.

Every birdcage was trial assembled as a complete 3.2-metre structure, then separated into four main panels plus the quartered top ring. Larger panels were nested around smaller panels for packing.

Approximately 50% less volumeAn estimated reduction achieved through nested modular packing.
Installation information suppliedNumbering and remote video guidance supported assembly by the client’s team.

A second project example

From rendering to illuminated cabinet.

The bar cabinet provides a direct visual comparison between the client-supplied rendering and the completed factory item. The 304 stainless-steel frame integrates an acrylic backing and concealed warm lighting.
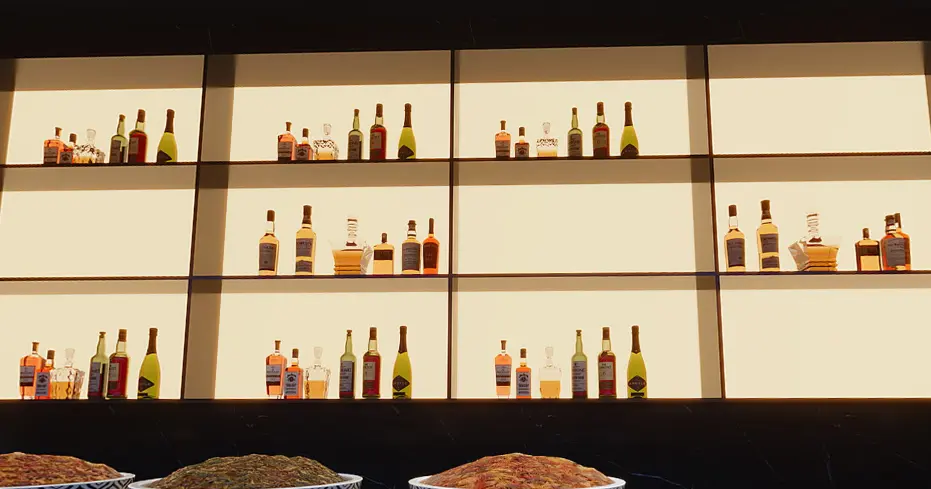
Client renderingClient rendering of the illuminated bar cabinet
Design input
Factory completedCompleted illuminated stainless-steel and acrylic bar cabinet in the workshop
Completed before shipment

Verification

Every assembly trial fitted before shipment.

All 67 assemblies were checked in the factory before protective EPE packing and sea shipment. Complex units were reassembled after surface treatment to verify that finish, geometry and connections still aligned.

Overall dimensions
Structural stability
Connection alignment
Surface finish
Glass and acrylic fit
Lighting function
Component numbering
Packing readiness
Finished & reassembledCompleted birdcage booth after rose-gold brushed finishing and final trial assembly
Project record: this case documents client design input and detailed workshop records through completion and shipment. Installation was completed by the client’s team with FABRITERA remote video guidance; completed-site photography is not currently available.
03 / Outcome

September 2026

Sixty-seven assemblies.
Ready in thirty-five days.

The full restaurant package was completed, checked and shipped by sea within the agreed 35-day period. The client handled local installation with remote video guidance from FABRITERA.

The completed delivery led to a further quotation request from the same client.

View all project case studies